A cogged belt fails early when tension, alignment, sheave condition, contamination, or installation is treated as guesswork. By the end, you will have a repeatable inspection routine, measurable tension and alignment checks, clear removal criteria, and a replacement checklist that prevents the wrong belt from entering the drive.
Key takeaways
- Isolate the drive with lockout/tagout before inspecting or servicing the belt.
- Use manufacturer tension values and investigate slip before adding tension.
- Correct misalignment, worn sheaves, oil contamination, and damaged belt teeth promptly.
- Verify belt profile, length, construction, and markings before ordering a replacement.
What should a cogged belt inspection routine include?
Build a cogged belt care routine around operating hours and the belt manufacturer’s instructions, then keep the interval consistent. Before hands-on work, isolate the drive under lockout/tagout. The guard must limit dust, oil, and accidental contact without blocking cooling or serving as a support for hoses or tools.
1. Record the date, drive identification, belt part number, tension reading, alignment result, sheave condition, contamination, temperature symptoms, and photographs.
2. Inspect every round for sidewall cracks or glazing, damaged or missing notches, frayed edges, exposed or broken cords, heat marks, oil swelling, hardening, chunking, tracking, slip evidence, and uneven width wear. Remove the belt for any of these defects when damage is severe, especially missing teeth or exposed cords.
3. Check the guard, grooves, and surrounding drive for contamination or conditions that caused the failure. Correct the initiating problem before fitting a replacement.
Store an unused cogged belt cool, dry, and shaded, away from ozone-producing equipment, sunlight, heaters, solvents, and other chemicals. Keep the product-specific temperature and humidity limits; relative humidity below about 70% is a common storage reference. Do not hang belts on small hooks or nails, fold them sharply, or bend them around a tight radius.
How do you set tension and separate slip from over-tension?
Measure belt tension across the specified free span, not at an arbitrary point. Use the manufacturer’s span-deflection method: identify the span, apply the stated force at its midpoint, and measure deflection. A calibrated tension meter is another option; hand pressure and visual sag are not measurements.
Use the drive or belt maker’s force or frequency value before any generic table. Make the first check after the drive has run briefly under load, because the belt can seat in the grooves and lose initial tension. Set the retensioning interval from the maker’s instructions and the drive’s load, geometry, and construction.
- Under-tension causes slip, squeal, glazing, and heat. Over-tension increases shaft and bearing loads and accelerates belt fatigue.
- Check for one-sided edge wear, wandering or poor tracking, and unusual noise before increasing tension. Those signs point to misalignment, not a tension shortage.
- If an industrial V-belt or industrial vee belts run hot, check insufficient wrap, overload, excessive speed, poor ventilation, belt slip, and an undersized sheave. Compare infrared readings with the belt compound’s operating limit and an equivalent drive.
- Do not use belt dressing to silence persistent squeal or cure glazing; it can contaminate grooves. Correct tension, alignment, sheave wear, overload, or contamination instead.
How should you inspect alignment and sheave condition?
Check alignment in two separate passes: face offset first, angular alignment second. Place a straightedge across both pulley faces, or use a laser, to identify offset. Then verify that the shafts and sheaves point in the same direction.
Parallel shafts with offset sheaves concentrate wear on the sidewalls; angular misalignment causes edge wear, tracking problems, and noise.
1. Lock out the drive and inspect the sheaves. Look for worn flanks, burrs, rust, oil or grease deposits, damaged groove surfaces, and an incorrect groove profile.
2. Check how the cogged belt sits in each groove. A belt sitting too low or bottoming out indicates a worn or incorrectly sized groove, not a tension problem.
3. Use a sheave-wear gauge or compare the groove with the belt and sheave manufacturer’s dimensions. Do not approve an industrial V-belt drive by eye alone.
4. Confirm that each sheave meets the belt profile’s specified minimum diameter. Cogged construction can permit a smaller sheave than some wrapped belts, but it does not make every undersized pulley acceptable.
5. Replace or machine a defective sheave before fitting a new belt. A new belt will reproduce the same wear pattern if the groove remains damaged.
What belt damage means the drive needs correction or replacement?
A damaged belt points to a drive correction, belt replacement, or both—not automatically to poor belt quality. Lock out the drive before inspection, then use this defect-to-cause checklist:
1. Replace the belt for cracked or missing notches, exposed tensile cords, chunking, severe fraying, hardening, or heat discoloration. Exposed cords require immediate removal from service.
2. Treat sidewall glazing and slip as drive clues. Check low tension, contamination, overload, insufficient wrap, excessive speed, poor ventilation, an undersized or worn sheave groove, and over-tension before installing another belt. Do not use belt dressing to cure squeal, slip, or glazing; it can temporarily alter friction and contaminate the groove.
3. Treat frayed edges, wear heavier on one side, and uneven wear across the width as alignment or sheave-condition clues. Correct face offset, angular alignment, burrs, rust, deposits, or an incorrect groove profile.
4. Remove belts with oil swelling or softened rubber, stop the leak, clean compatibly, and confirm the replacement compound suits the chemical exposure. Cogged belt care still follows industrial vee belts practice: a notched raw-edge V-belt remains a friction drive. Its notches reduce bending resistance and heat, but do not mesh with teeth.
A timing belt uses teeth, a matching pulley, and pitch, so it is not interchangeable.
Judge heat with the compound’s operating limit and a comparable reference; an infrared reading alone proves nothing.
How do installation, cleaning, and operating conditions affect service life?
Install a cogged belt with the motor or another adjustable center-distance component moved inward to create slack. Never pry an industrial V-belt over a sheave with a screwdriver, bar, or similar tool; the force can damage tensile cords and sidewalls before service begins.
1. Move the motor inward, fit the belt without force, then apply the specified tension. After installation, verify tension, alignment, and tracking before returning the machine to production.
2. Correct leaks before cleaning the drive, then remove deposits with a method compatible with the belt compound. Do not assume cogged construction resists oil, grease, solvent, coolant, or process chemicals. Swelling, softening, or cord-adhesion damage requires an oil-resistant or specialty compound confirmed for that exposure.
3. Keep the guard fitted without blocking ventilation, and never use it to support hoses or tools. If the belt runs hot, review load, speed, wrap, ventilation, ambient heat, contamination, slip, and sheave diameter instead of blaming the belt alone.
4. On a multi-groove drive, replace the complete set. Use matched lengths or a manufacturer-approved matched construction; never combine a new belt with visibly used belts or mix constructions without confirmation. Unequal lengths shift load onto fewer belts and shorten the set’s life.
How do you specify and verify the correct replacement belt?
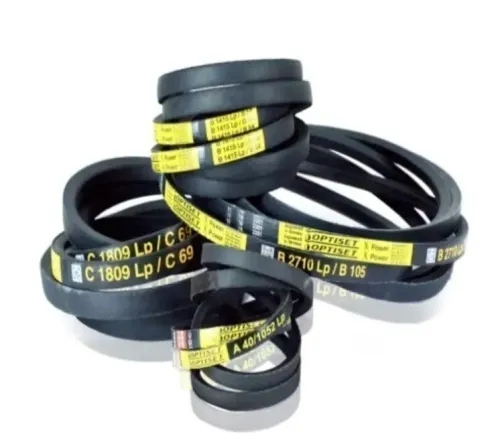
Specify the replacement by complete geometry and service conditions, not by “cogged belt” alone. Ask industrial v belt manufacturers to confirm the belt section or profile, construction, length convention, and whether the stated length is pitch or effective length rather than outside length.
| Item | Verify | Why it matters |
|---|---|---|
| Profile and construction | Section, wrapped or raw-edge cogged construction | Similar names can have different dimensions and tension behaviour |
| Length | Manufacturer’s convention: pitch/effective or outside length | The wrong convention produces a belt that appears close but will not tension correctly |
| Ribs and grooves | Required rib count; count the pulley grooves | A mismatch prevents even load sharing |
| Service conditions | Operating temperature, chemical exposure, and antistatic requirement where applicable | Heat or chemicals can damage an unsuitable compound |
| Drive arrangement | Matched-length requirement | Use a matched set; do not mix new and visibly used belts |
| Pulley geometry | Profile and manufacturer’s minimum diameter | A worn or undersized groove can damage the replacement |
Record the complete manufacturer part number, not “notched belt” or “raw-edge cogged belt.” If the groove no longer meets its specified dimensions, replace the pulley. Send the completed specification, old belt markings, drive speed and power, centre distance, and photographs to Jigna Sales Corporation for a like-for-like review.
Buy the belt that matches the drive, not merely one that fits over the sheaves.
Frequently asked questions
What should a cogged belt inspection routine include?
Inspect the belt for cracks, glazing, frayed edges, exposed cords, missing teeth, and oil contamination. Check tension, alignment, sheaves, guards, and unusual noise at a consistent operating interval.
How do you separate belt slip from over-tension?
Slip produces squealing, glazing, heat, and reduced driven speed. Over-tension causes excessive bearing load, rapid belt wear, and belt noise without correcting the underlying alignment or sheave problem. Use the manufacturer’s tension method instead of tightening by feel.
How should you inspect alignment and sheave condition?
Place a straightedge across the sheave faces or use a laser alignment tool. Look for angular or offset misalignment, worn grooves, burrs, rust, and debris. Replace damaged sheaves and correct shaft alignment before fitting a new belt.
What belt damage means the drive needs correction or replacement?
Replace a belt with cracked sidewalls, exposed cords, missing or damaged teeth, severe glazing, oil swelling, frayed edges, or chunks missing. Find and correct the cause, such as misalignment, incorrect tension, contamination, or an undersized drive.
How do operating conditions affect cogged belt service life?
Heat, oil, chemicals, abrasive dust, moisture, shock loads, and poor ventilation accelerate wear. Fit the belt material and construction to the environment, keep the guard clean, and prevent contaminants from reaching the belt.